

Product Overview
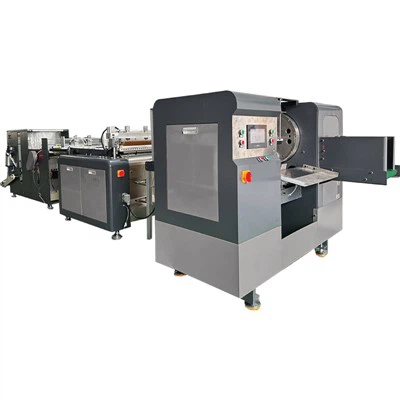
Jiuyi industrial plastic extrusion lines convert thermoplastic resins into continuous profiles, pipes, sheets, and films. Built for continuous multi-shift operation, each system integrates precision helical gearboxes, nitrided or bimetallic screw-barrel assemblies, and closed-loop PLC thermal control to maintain melt homogeneity and dimensional tolerance across high-output runs.
Engineered for processors running PVC, HDPE, PP, LDPE, ABS, and engineering plastics, these systems balance stable output rates with low specific energy consumption per kilogram processed.




Machine Types
Single Screw Extruders
Applied for general thermoplastic granulation, pipe extrusion (HDPE/PVC), and solid profile manufacturing. Features high L/D ratios (30:1 to 38:1) for thorough polymer melting and homogenization at steady line speeds.
Conical Twin-Screw Extruders
Engineered for rigid and plasticized PVC powder processing. Intermeshing counter-rotating screws deliver positive displacement feeding, minimizing shear degradation and thermal history for high-filler formulations.
Parallel Twin-Screw Extruders
Utilized for high-output compounding, masterbatch production, and reactive extrusion of engineering thermoplastics requiring rigorous degassing and additive dispersion.
Key Features
Helical Gearbox Drive: Hardened alloy steel gears ground to DIN class 6 accuracy, equipped with integrated thrust bearings to absorb high screw back-pressure while operating below 75 dB(A).
Bimetallic Screw & Barrel Assemblies: Base material 38CrMoALA furnace-nitrided to 0.6-0.8 mm depth (HV >= 950), with optional PTA alloy welded flights or centrifugal-cast bimetallic liners for abrasive or corrosive polymers.
Ceramic Band Heaters with Aluminum Cooling Jackets: Sectional thermal control paired with low-noise centrifugal blowers, maintaining PID temperature precision within +/- 1 degree C.
PLC-Controlled Synchronization: Siemens or Delta PLC and HMI architecture linking main drive inverter, feeder speed, melt pressure transducers, and haul-off motors to prevent gauge variation during speed ramps.
Technical Specifications
|
Model |
Screw Diameter (mm) |
L/D Ratio |
Max. Screw Speed (rpm) |
Output Range (kg/h) |
Main Motor Power (kW) |
Heating Power (kW) |
|
JY-SJ65 |
65 |
33:1 |
120 |
120-180 |
37 |
24 |
|
JY-SJ90 |
90 |
33:1 |
90 |
250-380 |
75 |
45 |
|
JY-SJZ65/132 |
65/132 |
- |
38.8 |
150-220 |
37 |
36 |
|
JY-SJZ80/156 |
80/156 |
- |
34.4 |
300-450 |
75 |
54 |
Municipal & Industrial Piping: Production lines for HDPE water/gas supply pipes (up to 1200 mm diameter), PVC electrical conduits, and corrugated drainage pipes.
Profiles & Construction: Window and door frame extrusions, PVC wall panels, cable trunking, and dual-durometer weather-seal gaskets via co-extrusion.
Sheet & Board Production: Extrusion of thick HDPE/PP geomembranes, thermoforming sheets, and wood-plastic composite (WPC) decking boards.
Compounding & Pelletizing: Strand pelletizing and water-ring face-cutting lines for virgin polymer coloring, filler masterbatching, and recycling.


Screw Geometry Modification: Custom compression ratios, barrier flight designs, and mixing sections (Maddock or Egan) tailored to specific MFI values and filler percentages (e.g., CaCO3 up to 70%).
Co-Extrusion Integration: Addition of secondary satellite extruders for colored striping, skin-core structures, or UV-resistant protective layers.
Voltage & Utility Alignment: Electrical configurations built to local industrial standards (e.g., 380V/50Hz, 480V/60Hz, 600V) with UL or CE-compliant components.
Downstream Equipment Matching: Vacuum calibration tanks, caterpillar haul-offs, planetary saws, and stacking tables engineered to match line throughput.
Company Advantages
Vertical Component Control
In-house machining centers handle critical structural elements including barrel boring, gearbox housing milling, and screw flight profiling, securing dimensional repeatability across batches.
Transparent Engineering Data
Complete electrical schematics, hydraulic diagrams, PLC source code access (upon request), and part interchangeability lists supplied with every machine.
Application Testing Facilities
In-house trial plant equipped with full-scale extrusion lines to run material trials using client-supplied resin batches prior to shipment.
Manufacturing & Quality Control
Dimensional Inspection
Screw straightness verified on CMM inspection tables; runout tolerances held within 0.03 mm across total length.
Metallurgical Testing
Spectrogram analysis performed on incoming alloy steel bars to verify carbon, chromium, and molybdenum percentages against material certifications.
Load Testing
Every assembled extruder undergoes a 4-hour dry-run factory acceptance test (FAT) measuring vibration amplitude, bearing temperature rise, and motor current draw under variable load steps.
Installation & After-Sales Support
Commissioning Engineers
Field service technicians available for on-site mechanical alignment, utility connection verification, and initial trial runs.
Remote Diagnostics
Ethernet-enabled control panels allow secure remote PLC connection for firmware updates and parameter tuning.
Spare Parts Inventory
Standard wear components-including heater bands, thermocouple probes, pressure sensors, and drive belts-stocked for immediate dispatch to minimize line downtime.
FAQ
We're professional plastic extrusion machine manufacturers and suppliers in China, specialized in providing high quality customized service. We warmly welcome you to buy high-grade plastic extrusion machine from our factory. Contact us for quotation.
plastic moulders, plastic thermoforming machine, polystyrene extrusion